
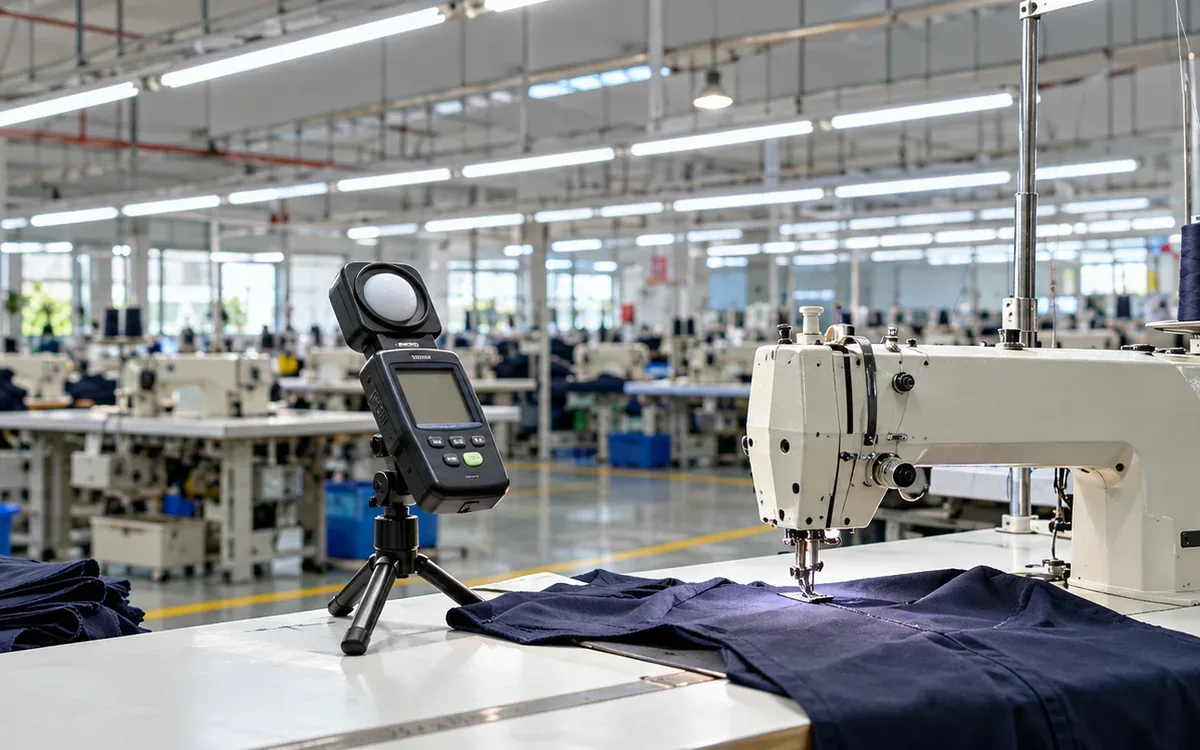
Audit the work surface, not just the light fitting
Ceiling lights may look bright. A sewing operator can still struggle to see a dark seam. A cutting table may have a good average lux value but a dim edge. A packing bench may look bright until a carton blocks the task light. These are lighting problems that a fixture count will miss.
A garment factory lighting audit should link three records. The first describes the visual task. The second measures the light that reaches it. The third measures the energy used by the lighting system. Together, they support a useful retrofit decision.
Begin at the workstation. Watch the normal task and ask where visibility changes. Note the material colour, surface finish, hand position, and line of sight. Then decide which measurements can test the reported problem.
This guide covers production lighting and retrofit checks. Controlled colour approval has a separate purpose. Use ApparelDiary's fabric colour approval guide for that process. A general factory lighting upgrade does not replace an agreed colour-viewing setup.
Define a requirement for each task
Do not copy one lux target across the whole building. Reading a carton label differs from sewing a dark seam. Checking a small surface flaw is another visual task. The task surface and the surrounding area both matter.
Identify the applicable workplace rules and lighting standard with the responsible designer. Add buyer requirements where they apply. Record the exact task, target, and measurement plane. State the uniformity criterion. Is the value initial or maintained? Retain the edition and source of each requirement.
The ILO's Ergonomic Checkpoints treats task needs, local lighting, glare, and light distribution as related issues. Its examples include precision work and dark materials. Use that task-based approach to frame the survey.
Work area | Main audit question | Surface to identify |
|---|---|---|
Sewing station | Can the operator see the seam and guides? | Actual needle and material work plane |
Cutting table | Is the full cutting area usable? | Table surface, including edges |
Inspection station | Are relevant flaws visible under the approved setup? | The actual inspection surface |
Packing bench | Can staff read labels and check packing details? | Bench and label-facing plane |
Storage aisle | Can staff read stock and move safely? | Relevant vertical faces and travel area |
Include people who use the space in the review. A survey performed with empty benches can miss shadows from normal work and stock.
Know what lux does and does not measure
Illuminance describes light arriving at a surface. Its unit is lux, equal to a lumen per square metre. The CIE definition of illuminance sets out this surface-based quantity.
A lamp's lumen output is different. It describes emitted light, not how much reaches a seam. Mounting height, optics, spacing, dirt, and room surfaces affect the light at the task. A more efficient lamp may send light to the wrong place. Task lighting can still be poor.
Lux also does not describe every part of visual quality. Glare, contrast, colour rendering, and changes in light over time need other evidence. A bright reflection may raise the meter reading. Yet it can make a defect harder to see.
Keep electrical watts separate from lumens and lux. Watts measure input power. Lumens measure light output. Lux measures light on the task. The audit needs the appropriate value for each question rather than a single “brightness” number.
Build an inventory that matches the circuits
Give each lighting zone a code on the floor plan. Record fixture type and quantity. Identify the lamp or module and its driver or ballast. Add rated input, control group, and mounting. Note failed units, dirty lenses, damaged covers, and changed fittings.
Distinguish lamps from complete fittings. Two tubes may each be marked 32 W. The complete input may exceed 64 W because the ballast also uses power. An LED module rating may also differ from the whole fitting's input.
Map circuits to zones. One feeder may include fans, sockets, or emergency chargers as well as general lights. A feeder meter is useful only when its loads are known. Identify which circuits stay live during dimming or an apparent off state.
Record operating schedules from evidence. A posted shift plan may miss some use. Cleaners may switch on early. Packing may continue late. Use logs or metering for the hours that matter to the savings estimate.
Keep photographs with the internal audit record. Include the fitting label and its position. This helps prevent a quoted replacement from being compared with the wrong installed product.
Prepare the lux measurement
Use a meter suited to the light source and required accuracy. Record its identity, range, calibration status, and stated limitations. Follow the maker's method for orientation and use. A phone reading may locate a dark spot. Validate it before using it for formal acceptance.
Identify the task plane before taking readings. Keep the sensor at that plane and orientation. Do not measure above the cutting table for convenience. Measure at the actual task surface.
The CIE definition of average illuminance requires the relevant surface orientation to be clear. A horizontal reading does not describe light on a vertical label. Record which one was measured.
Allow the lighting to reach the state required by the test method. Set the control mode deliberately. Record daylight, blind position, fixture status, and any local task lamps. Avoid shading the sensor with the surveyor's body.
Save all readings, not only the average. Keep time, location, and test state with each value. Those details make a later comparison possible.
Resolve a reading close to the limit
Suppose a hypothetical acceptance point needs at least 500 lux. The meter shows 510 lux, with a stated uncertainty of ±4% for the actual test. That range extends below 500 lux. The reading alone does not support an unqualified pass.
Agree how such cases will be decided before testing. A better measurement, a design margin, or an agreed decision rule may resolve the issue. Repeating a reading many times does not remove a shared calibration bias.
Keep changes in daylight separate from meter uncertainty. If readings move as clouds pass, the source itself is changing. Record that change and choose conditions suited to the acceptance question.
Use a repeatable grid
Choose the grid from the adopted method and the area being assessed. Mark each point on the layout. Keep the same grid before and after a retrofit unless the task area itself changes. Document any necessary change.
An equal-area grid lets an arithmetic mean represent the sampled area. If points represent unequal areas, use appropriate weighting. Do not crowd the grid beneath one bright fitting. Include dim edges in the planned pattern. Each point must represent its stated area.
Measure a whole task area. A single spot beneath a lamp can conceal poor edge lighting. Check adjacent work areas too. Moving a fitting may improve one bench but make its neighbour worse.
Keep the normal work arrangement in view. Record whether the operator, machine head, guard, or material shades the task. A defined unoccupied measurement and an occupied task check answer different questions. Retain both when needed.
For long production lines, select representative positions and known problem spots separately. Do not use only complaint locations to estimate the whole line average. Do not use only easy locations to declare all stations acceptable.
Calculate average light and uniformity
The CIE illuminance uniformity definition uses minimum illuminance divided by average illuminance on the surface. Write this as U₀ = Emin ÷ Eavg. It has no unit.
The following nine-point grid is hypothetical. Each point represents equal area on one task surface. The “after” readings follow a layout trial.
Point | Before, lux | After, lux |
|---|---|---|
1 | 620 | 640 |
2 | 580 | 620 |
3 | 540 | 610 |
4 | 600 | 630 |
5 | 560 | 620 |
6 | 500 | 600 |
7 | 580 | 620 |
8 | 520 | 600 |
9 | 400 | 580 |
Before average = 4,900 ÷ 9 = 544.44 lux.
Before uniformity = 400 ÷ 544.44 = 0.735.
After average = 5,520 ÷ 9 = 613.33 lux.
After uniformity = 580 ÷ 613.33 = 0.946.
Assume the initial trial target is 600 lux. The project also requires U₀ of at least 0.80. These are invented targets for this example. The trial meets both; the original arrangement meets neither.
The result does not establish long-term compliance. It also does not test glare or flicker. It shows why the average and minimum should be reviewed together.
Distinguish initial from maintained light
Initial readings describe a defined new or clean condition. A maintained-light requirement applies as the system ages and gets dirty. It defines the light that must still be available. The two values should not be exchanged without explanation.
A design may apply a supported maintenance factor to estimate future illuminance. Suppose a hypothetical design needs a maintained average of 600 lux. If its justified maintenance factor is 0.80, the calculated initial average is:
Initial average = 600 ÷ 0.80 = 750 lux.
The 0.80 factor is an assumption here. It must come from the actual products, environment, and maintenance plan in a real design. It is not a standard value for every garment factory.
The earlier 613.33-lux trial would yield only 490.67 lux after applying that assumed factor. It met its stated initial trial target but would not meet this different maintained-light design case. Keep the two decisions separate.
Overlighting a new area is not the only response. Suitable controls can hold the required level as output changes. A cleaning and replacement plan can also affect the supported factor. Ask the designer to show the basis rather than add an unexplained margin.
Diagnose shadows and glare at the task
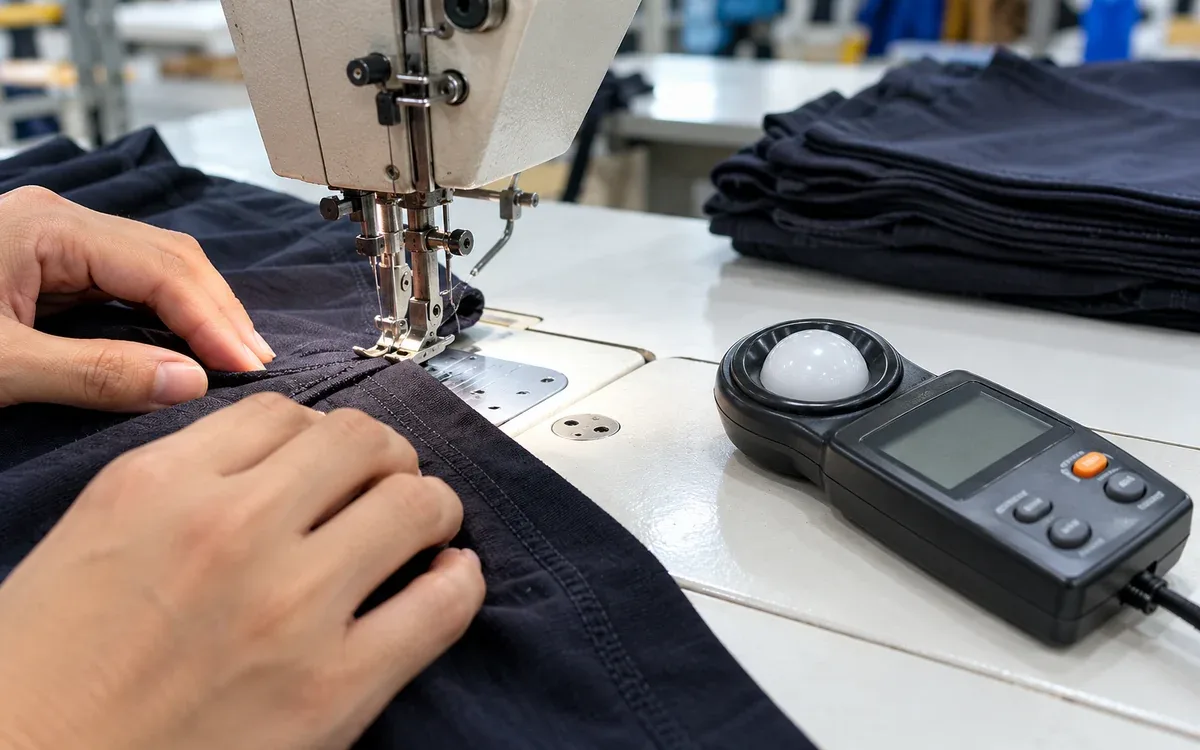
Sit or stand where the task is done. Observe the seam, tool, label, and screen from the normal line of sight. A surveyor standing beside the bench may miss the reflection seen by the operator.
Check whether hands or machine parts block the light. Test a different lamp position before increasing its output. A small angle change may improve the view without adding power. Keep the new position clear of moving parts and normal handling.
Look for bright sources directly in view. Also inspect reflections from polished tables, metal parts, screens, and shiny fabric. Shielding, optics, surface finish, or layout may need adjustment. A diffuser can alter both glare and useful light, so remeasure after the change.
Record the problem in task terms. For example, record that a bright reflection hides the seam guide. State the seated viewing position. This gives more detail than “lighting is harsh.” It tells the designer what a correction must prove.
Do not treat a low-glare product label as proof of a good installation. The installed geometry, room, and observer position affect the result. Obtain the relevant design check and inspect the actual pilot area.
Check light changes over time
Some lighting varies rapidly in output. The visible effects depend on the waveform, equipment, movement, and observer. A light that looks steady to one person may still create a problem for a task.
DOE's flicker research distinguishes direct flicker, stroboscopic effects, and phantom-array effects. It also explains why one metric cannot describe every application. Ask for suitable test evidence at the actual operating settings.
Check the full control range, not just full output. Dimming can change the behaviour of a driver and light source. Confirm compatibility among the fitting, driver, and control system.
CIBSE's temporal-lighting factfile notes the risk of moving equipment appearing stationary under stroboscopic effects. Include the safety team when assessing lighting near moving machinery. Do not use visual appearance to decide that equipment has stopped.
A phone video may reveal a symptom but does not replace suitable measurement. Camera exposure and frame rate can alter the recorded pattern. Use the relevant method and instrument to resolve an acceptance question.
Keep colour requirements specific
Correlated colour temperature describes one aspect of the light's appearance. A matching CCT does not prove that two sources have the same spectrum or colour rendering. Do not buy an inspection light from its Kelvin value alone.
Define what the station must do. General handling, defect detection, and formal shade approval may need different evidence. Use samples that reflect the production work. Include dark and reflective materials where relevant.
If a buyer has an approved viewing method, keep it intact. A ceiling fitting may claim high colour rendering. It does not replace the required illuminants, viewing geometry, or procedure. Link the lighting asset record to the actual approved use.
Record changes in product and driver codes. A replacement that fits the same housing may have different light properties. Maintenance needs a controlled replacement list, not just a wattage and socket description.
Calculate retrofit energy from complete input
Assume a hypothetical factory has 200 fittings. Each existing fitting draws 72 W including its ballast. Each proposed fitting draws 38 W at full output. Both arrangements provide the required lighting service. Annual scheduled operation is 3,600 hours.
Existing energy = 200 × 72 ÷ 1,000 × 3,600 = 51,840 kWh/year.
New full-output energy = 200 × 38 ÷ 1,000 × 3,600 = 27,360 kWh/year.
Before adding controls or standby loads, the calculated reduction is 24,480 kWh/year. These input values need measurement or suitable product evidence in a real project.
Use whole-system power. Do not compare old lamp watts with new fitting input. Check the installed quantity after layout changes. Count new task lights and any separate drivers.
Keep useful light as an acceptance condition. A lower-wattage option may leave the area below its light requirement. It is then not an equivalent saving. Revise the design or define the service change openly.
Add controls without double counting savings
Suppose the new system's measured average power during scheduled hours is 72% of its full-output power. This factor represents the combined effect of its controls under the assumed duty.
Controlled operating energy = 27,360 × 0.72 = 19,699.2 kWh/year.
A 365-day year has 5,160 hours left outside this schedule. Assume each fitting draws 0.4 W during those standby hours. Standby energy is:
200 × 0.4 ÷ 1,000 × 5,160 = 412.8 kWh/year.
New total = 19,699.2 + 412.8 = 20,112 kWh/year.
Total saving = 51,840 − 20,112 = 31,728 kWh/year.
Do not add a claimed occupancy saving and daylight saving as independent percentages if they overlap. The combined measured factor already contains their joint effect.
The DOE guidance on advanced lighting controls covers energy measurement, control performance, and user experience. It highlights the need to consider operating conditions and daylight variation. Use representative periods rather than extending one unusually bright day across the year.
Test controls with people doing real work
An occupancy sensor can miss someone who remains still while sewing or inspecting. It can also respond to movement outside its intended zone. Test its coverage with the actual work pattern.
Set delays and dimming levels with the task and safety requirements in mind. Test arrival, quiet work, departure, cleaning, and restart after power loss. Check manual override and restoration. Record settings that maintenance can reproduce.
For daylight control, locate the sensor so it represents the zone. Confirm that blinds, stock, and machine layout do not defeat it. Check both window-side and inner workstations as daylight changes.
Separate control commands from real input power. A 50% dimming command may not mean 50% electrical power or 50% task illuminance. Measure the relevant relationship for the installed system.
Keep essential and emergency lighting functions within their approved design. A general energy-control change should not silently alter those functions. Have the responsible electrical team confirm the circuit and control arrangement.
Price the saving with explicit assumptions
Use the hypothetical saving of 31,728 kWh. Assume an avoidable price of 0.12 currency units per kWh. Annual energy value is 3,807.36 currency units.
If installed project cost is 14,000 currency units, simple payback is:
14,000 ÷ 3,807.36 = 3.68 years.
This is a teaching example, not a market quotation. It excludes financing, taxes, changing tariffs, and maintenance differences. It also excludes unproved productivity benefits.
Include added task lighting. For example, 40 new task lights at 6 W for 3,600 hours add 864 kWh/year. Net savings would then fall to 30,864 kWh/year if nothing else changed. Small loads still belong in the defined boundary.
Assess demand charges from the actual tariff and timing. Lower lighting power may not reduce the billed peak by the same amount. For a fuller investment review, use ApparelDiary's factory cash-flow guide.
Run a pilot before the full order
Select a pilot area that represents demanding work. Include typical materials, operators, and neighbouring stations. Test the proposed fitting and controls in their intended positions.
Use the same measurement grid and methods as the baseline. Add a task trial with known samples where appropriate. Keep the sample order varied so memory does not dominate a defect-detection comparison. Record false accepts and false rejects separately.
Do not promise a productivity increase from worker preference alone. Preference is useful evidence, but output and quality need their own controlled comparison. Training, style, machine condition, and work pace can change those results.
Inspect the pilot after normal cleaning and use. Check mounting, heat, access, dirt accumulation, and accidental adjustment. A fitting may work well on day one. Check how staff will maintain it above a busy line.
Resolve complaints before placing the main order. Keep the approved product code, optics, driver, control version, and settings. Otherwise, the bulk installation may differ from the successful pilot.
Make acceptance and maintenance measurable
Write the acceptance plan before installation. Include task illuminance, uniformity, glare review, relevant colour evidence, temporal-light performance, electrical input, and control operation. State which requirements come from a standard and which are project decisions.
Inspect installation quality with the responsible specialists. Verify product identity and approved wiring. Record substitutions and obtain their technical review. A similar-looking fitting is not automatically equivalent.
Set a cleaning and remeasurement plan based on the site. Use the same reference points to track change. Recheck after line moves, partition changes, or repeated fitting failures. Keep a record of both the clean condition and the as-found condition where useful.
Store the audit map with maintenance records. A new operator or engineer should be able to find the same point without guessing. The value of a lux trend depends on that repeatability.
Frequently asked questions
Is more lux always better?
No. The task needs sufficient light with suitable distribution and low interference from glare. Extra output may waste energy or create reflections. Assess the actual work and the adopted criteria.
Can one reading approve a sewing line?
One reading describes one point at one time and condition. A line needs a suitable sampling plan, including variation along the work area. Retain the minimum and distribution as well as the average.
Does a high CCT prove good colour inspection?
No. CCT alone does not define the spectrum or the viewing method. Use the required colour evidence and maintain any approved colour-assessment setup.
Can catalogue watts prove annual savings?
They can support a preliminary estimate. Confirm whole-fitting input, quantity, operating hours, control states, and standby loads. Verify that the new system meets the required lighting service.
Conclusion
Start the garment factory lighting audit with the task. End with an acceptance record that others can repeat. It measures the right surface and checks uneven light and glare. It tests controls in use. It also counts all relevant electrical loads.
Use a pilot to connect the design with real production. Keep the approved layout and product details with maintenance records. The factory can then preserve visual quality. It can also track energy savings on a sound basis.
References
ILO, Ergonomic Checkpoints, second edition.
CIE, Illuminance, e-ILV 17-21-060.
CIE, Average illuminance, e-ILV 17-29-155.
CIE, Illuminance uniformity, e-ILV 17-29-160.
CIBSE, Temporal Lighting Artifacts, Lighting Factfile 17, 2021.


Discussion0
Loading the discussion…