
Use evidence to replace the process
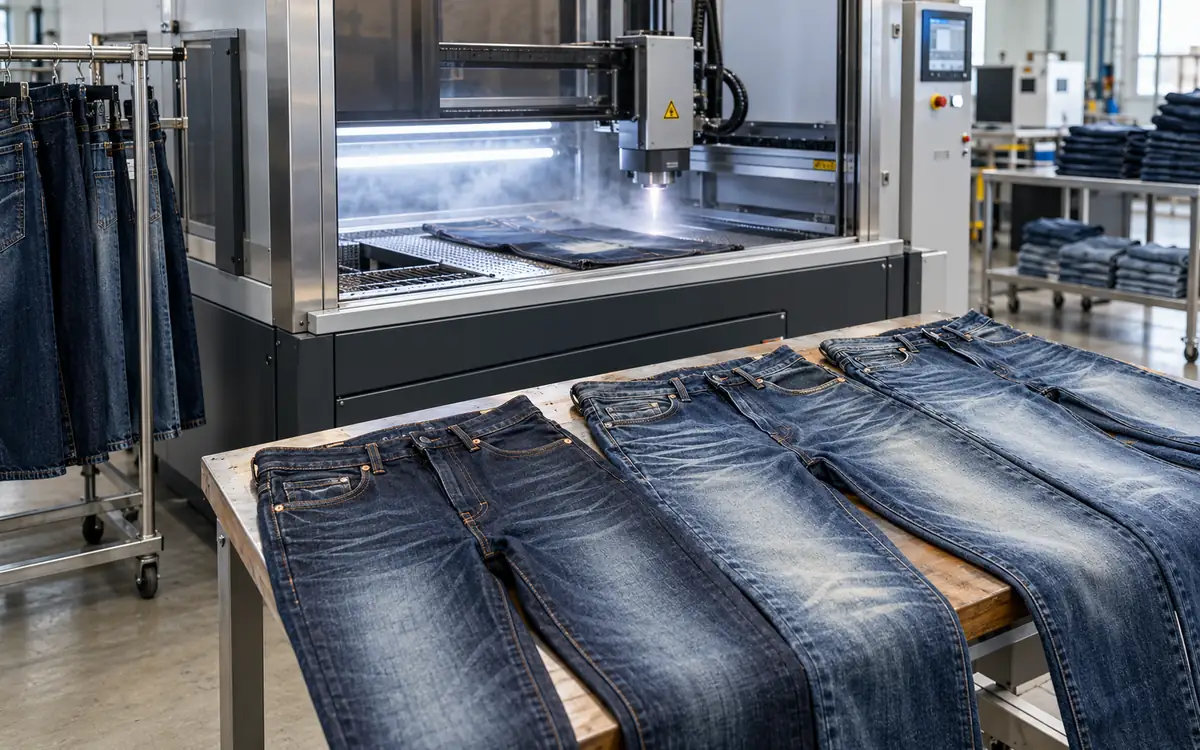
Denim sandblasting directs abrasive particles at the garment to create a worn look. The material may contain respirable crystalline silica. Dust from this material can cause severe lung disease. NIOSH explains that silicosis is irreversible but preventable.
A project to replace the process must answer a few key questions. Can the new route make a garment that meets the brief? Does it remove the old exposure? Are any new hazards well controlled?
Buying a machine answers neither question on its own. New technology can still need dust or fume control. It also needs safe maintenance and trained staff. A good-looking sample can hide weak fabric. It can also hide work done by a finisher outside the approved route.
Treat replacement as a clear change in the finishing route. Name the old process and the intended product result. List the proposed options and the evidence needed for release.
This guide focuses on that decision and changeover. Keep laser, ozone and wet-process settings in their own records. These should cover equipment and product trials and approval.
State what the health evidence shows
The danger of denim sandblasting is well documented. Akgun and colleagues followed former denim sandblasters for four years. Their study recorded serious disease progression after exposure had stopped. The study followed a defined group of workers. Do not use its results to predict what will happen to each individual worker. Read the primary study in CHEST.
Stopping exposure does not erase earlier harm. The factory should arrange suitable occupational-health follow-up for affected workers. Qualified clinicians should guide this care under the rules that apply.
Do not ask production staff to judge a worker’s health from visible symptoms. A workshop may look clear. That is not evidence that past or current exposure is harmless.
Keep health records private. Store them apart from commercial trial results. The buying team needs to know that worker health care is in place and well managed. It does not need each worker’s medical details.
A replacement plan can improve future conditions. It must also recognise duties that remain from the previous process.
Check buyer rules before choosing a method
A legal rule, a buyer requirement and a factory policy are different documents. Name each one and record what its current version covers.
For example, the Levi Strauss 2025 supplier implementation guide bans all forms of abrasive blasting. It requires suppliers to remove related equipment and materials. The ban includes listed alternatives to silica sand. This is a buyer requirement. It is not a law that applies in every country.
That distinction changes the shortlist. A new grit may contain less silica. That alone cannot meet a buyer’s ban on the blasting process.
Ask whether the buyer’s rule covers manual and automated blasting. Check if it covers all media, sample development and work sent to outside finishers. Get the requirement through the normal approved document channel.
Record the edition and review date. An old approval does not override a current restriction.
If a process is prohibited, remove it from the production route. Do not keep it as an emergency option while testing a replacement.
Define the look that the new route must keep
“Match the old sandblast” is an incomplete development brief. Split the look into features that a buyer can assess.
Record the location of the light area, edge softness and contrast. Add visible yarn texture and the way the effect relates to garment seams. Some features may be essential. Others may be open to redesign.
Use an approved physical sample where possible. Mark which areas may differ when the route changes. A product team may accept a revised fade pattern if the overall design remains right.
Write those decisions before comparing technologies. Otherwise, every trial can be rejected for a different reason.
Design feature | Question for approval |
|---|---|
Location | Must the effect align with a fixed garment landmark? |
Edge | Is a soft transition essential, or is a clear border acceptable? |
Contrast | Which zones must remain dark or become light? |
Texture | Must yarn texture remain visible after finishing? |
Damage | Are holes or broken yarns prohibited in the effect zone? |
Variation | How much natural-looking variation is permitted? |
This brief lets the team change the method and keep control of the product.
First ask if the stage can be removed
The first option is to remove the need for the harmful step. Could the garment use a different fabric, a less extreme worn effect or a revised design?
NIOSH’s hierarchy of controls puts elimination and substitution first. These rank above controls that depend heavily on worker behaviour. It also calls for a review of new risks from a substitute.
For denim, a design change may reduce the amount of finishing needed. Trial that option alongside new equipment.
This does not mean that every collection must use a plain dark jean. The design team needs to understand the real limits. It can then help choose an effect the factory can achieve.
Document what is removed from the route. A revised fabric may reduce one local abrasion stage but add a chemical operation. Include the new operation in the comparison.
A design change may need buyer approval or fabric development. It may also need a longer lead time at first. Those are planning issues. Include them in the decision. They are not a reason to dismiss the option without review.
Compare what each option does and which hazards remain
Several types of process can help create a worn denim effect. The best choice depends on the intended result and the complete route.
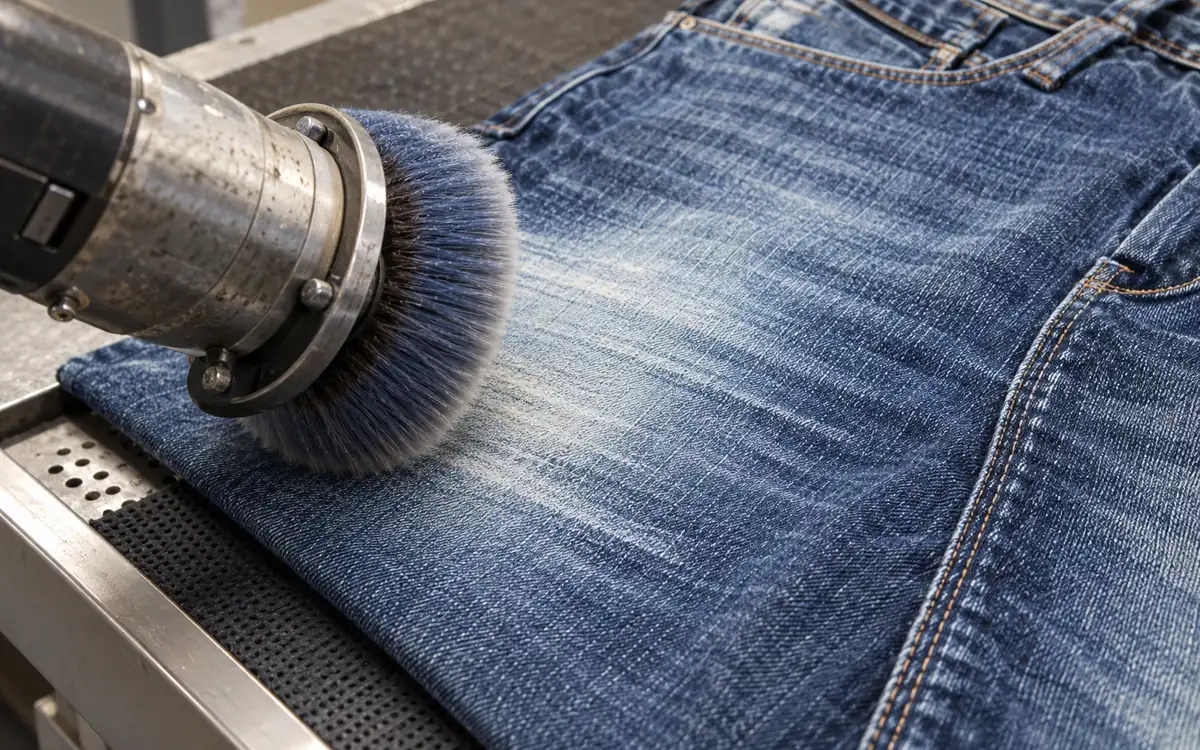
Jeanologia offers laser equipment for denim marking. Tonello offers manual brushing equipment. These sources show that such options exist. They do not independently prove that a factory installation is safe. Nor do they approve its garment result.
Candidate route | Potential role in the design | Questions still requiring evidence |
|---|---|---|
Revised fabric or effect design | Reduce or remove local distressing | Buyer acceptance and fabric performance |
Enclosed laser route | Produce controlled local patterns | Emissions control, guarding and fabric damage |
Controlled brushing or sanding | Create local surface wear | Dust, posture, repetitive work and consistency |
Enclosed ozone route | Change shade or selected effects | Gas containment, access control and material response |
Qualified wet finishing route | Develop wash-down or overall character | Chemical hazards, discharge and garment performance |
Combined route | Divide the visual task between methods | Total exposures, handoffs and cumulative damage |
A combination may be needed. Assess the combination as one route, including any manual touch-up.
Check the new route for all hazards
A “silica-free,” “waterless” or “chemical-free” claim answers one narrow question. It does not prove that the whole process is safe.
A grit with no silica may still produce dust. A process that uses heat may release fumes or other emissions. A wet process may involve hazardous substances or hot handling. Manual finishing can add physical strain even when it uses few chemicals.
The EPA’s alternatives-assessment approach looks at a broad range of health and environmental hazards. The aim is to avoid new problems from a substitute. Apply that principle to the complete denim route.
Ask what material enters the process and what leaves it. Find out who may come into contact with either. Include normal work and cleaning. Add filter changes, repairs and waste handling.
Ask for evidence for the actual product and working conditions. A machine may have safety evidence for one fabric. That does not cover every coating, blend or finish.
Use ApparelDiary’s HIRA guide to organise the site assessment. The team still needs evidence for the specific finishing tasks it proposes.
Set firm pass conditions before comparing cost
Some rules must be met even if another option is cheaper or faster.
Set mandatory pass conditions for process bans and essential engineering controls. Add serious exposure concerns that remain unresolved. The garment must also meet its minimum test limits. An option that fails one of these checks remains unapproved.
Then compare the candidates that pass. Compare cost, repeatability and service support among routes that pass. Consider how well each can meet changing delivery needs too.
A weighted score alone cannot resolve a critical failure. A low price should not offset missing exposure evidence in the score.
For each check, state the evidence needed. Name the person who makes the decision. “Safety approved” is too vague on its own. The team must be able to name the assessment, approved uses and required controls.
Use “evidence incomplete” when needed. It differs from both “pass” and “fail.” This stops the team from treating missing data as a favourable result.
Do not release commercial production while a mandatory check is incomplete. Resolve it or choose another approved route.
Build trials around garments that represent production
Choose garments that test the limits of the new route. Include the dyes and fabric types that the route needs to handle.
A trial set might contain a rigid dark denim, a stretch style and a garment with sensitive trims. Include sizes or placements that are likely to make the effect difficult.
Use a consistent starting state. A washed garment and a raw garment start in different states. Their comparison is fair only if that difference is part of the planned route.
Keep a reference garment. Save samples from each proposed route. Record the exact sequence used. Include all touch-up and final washing.
Measure the garment after the complete route. A good effect at one stage can change during later treatment.
Plan enough pieces to assess appearance and run destructive tests. Allow for repeat runs too. Do not use the single best sample as the only basis for approval.
Record which pieces pass the first time. Keep successful repairs separate from that count. A route may need several rounds of correction. That can add new exposure and quality demands.
Check exposure during the real work
Assess exposure during the tasks people actually do. Have a competent occupational hygienist or other qualified specialist carry it out.
Include operators and nearby workers where relevant. Cleaners and maintenance staff may also need to be covered. The main machine cycle may be enclosed. Loading or waste removal can still create a different exposure.
The specialist should choose suitable sampling methods and locations. They should also set the sampling time and the rules for judging results. A general dust reading may not show how much of a specific harmful substance is present.
Record which conditions the assessment covers. Include material, workload and equipment state. Add controls and task duration. A quiet demonstration period may not represent a busy shift.
If a result is below the reporting limit, state that limit. It does not prove that the substance is absent.
If the new route adds a different hazard, assess it directly. Do not use the absence of silica as proof that all other risks are controlled.
The report should state the conditions in which its findings apply. It should also say which changes need a new review.
Give the garment and exposure review separate approvals
Product approval and exposure approval are both required. Neither replaces the other.
For the garment, review appearance, dimensions and relevant strength. Check seams, trims and care performance too. Select the tests from the product’s use and construction.
Pay close attention to the zones with the strongest effect. A test taken only from a protected area may miss damage in the visibly worn area.
Use the same sampling logic for competing routes. If one route is tested at the knee and another near the hem, the results may not support a fair comparison.
Check the final test limits. Also compare the change from a suitable control. A retention percentage can help explain the effect. The minimum test limit still applies.
For example, take a hypothetical garment test with a result of 800 N before finishing. The result is 680 N after a candidate route. Retention is 680 ÷ 800 × 100 = 85%. Suppose the agreed minimum is 700 N. The route retains most of the original value but still fails this requirement.
Work through a replacement decision
Consider three hypothetical candidates for one approved denim effect. The factory has already removed sandblasting from the approved route.
Criterion | Candidate A | Candidate B | Candidate C |
|---|---|---|---|
Buyer process restriction | Pass | Pass | Fail: abrasive blasting remains |
Required exposure evidence | Complete and accepted | Incomplete for manual touch-up | Not assessed further |
Garment appearance | Pass | Pass | Pass |
Minimum performance tests | Pass | Pass | Pass |
Decision | Eligible for controlled release | Hold for evidence | Reject for this buyer |
A better cost score cannot make Candidate C acceptable. Candidate B needs more evidence, even though its sample looks right.
Suppose Candidate A costs 1.80 currency units per attempted garment. It has a 96% first-pass accepted share. Its simple processing cost per first-pass accepted garment is:
1.80 ÷ 0.96 = 1.875 currency units
A second fully approved route costs 1.65 per attempt but accepts 88% first pass:
1.65 ÷ 0.88 = 1.875 currency units
On this narrow measure, the lower unit price gives no cost advantage. Count rework, capital and maintenance costs separately. Other costs may also apply. These figures are examples. They are not market prices or a full investment appraisal.
Buy the complete new system
Define the replacement as an installed process. Buying only a machine may leave out essential parts of that process. The order should state what it includes for emissions control and material handling. Add waste collection and commissioning.
Ask who will connect each part. A supplier may assume the factory provides extraction. The factory may assume it comes with the machine. That gap can leave a trial unable to proceed.
List the evidence needed before the factory accepts the system. It may include installation checks and tests of control functions. Add operator training and the agreed product trial. Competent specialists should set the technical requirements for their own areas.
List recurring tasks too. Filters, sensors, seals and other parts may need checks or replacement. Budget for those tasks before comparing operating costs.
Plan what to do if the system fails. If the replacement system stops, use an approved backup route or hold procedure. Identify these in advance. The backup must meet the same firm pass conditions. It must not bring back the old process.
Keep any excluded supply items visible in the order. A price may leave out essential controls. It cannot be compared directly with a complete installed offer.
At handover, give production, maintenance and safety staff the same approved scope. This helps protect controls required for the original release. A later repair or cost cut must not remove them.
Include hand work in the approved route
A replacement may appear successful because its hardest work has moved to a side table.
Observe what happens after the main machine cycle. Are workers brushing missed areas or spraying marks? Are they grinding edges or correcting mismatched pairs? Those tasks belong in the route assessment.
Record how often these tasks occur and how long they take. Include the materials used, the workstation and the controls. A rare repair has a different effect on production from a correction made on every piece.
Use defect records to decide if the main process needs to change. Review any rise in manual correction as order pressure grows.
If a task is outside the approved route, review it before adding it. A spoken instruction from a supervisor should not create a new process.
This is also a quality issue. Uneven touch-up can make the buyer’s sample hard to repeat. It can also weaken parts of the garment.
Plan a changeover that cannot drift back
Set a dated changeover plan with named owners. List open orders and work in progress. Include sample requests and quantities sent to outside finishers.
Move each affected style to an approved route or obtain an approved design change. If neither is ready, hold the affected work. A delivery problem does not justify returning to a banned process.
Control old instructions, artwork labels and routing codes. A process can remain in use because an old job card still asks for it.
Account for all pieces at changeover. Take a hypothetical order for 2,000 pieces. There may be 500 awaiting finishing, 900 on an approved new route and 600 already complete. The status total should equal 2,000. Record a clear decision for each group.
Keep production status separate from compliance status. “Completed” alone does not prove that a garment followed an approved route.
Use the transition record to prevent mixed batches and unclear product claims.
Retire old equipment and handle what remains
Stopping new work does not remove old dust or abrasive stock. Contaminated equipment remains too.
Have competent staff plan how to retire the equipment, clean it and handle waste. Follow the rules that apply. The plan should cover equipment interiors and collection systems. Add storage areas and other places where residue may remain.
Do not improvise cleaning methods that spread dust or other contamination. Routine housekeeping alone does not prove the area is ready for unrestricted use.
Record the equipment’s identity and what happens to it. Name the contractor or team responsible. A buyer may require removal. If so, keeping an unused machine on site may still fail the rule.
Account for the remaining abrasive stock. A record may show no new purchases. That is not enough if a large old stock remains available.
Keep disposal and transfer evidence that suits the materials and local rules. End the process without passing an uncontrolled hazard to another person or location.
Check outside finishers and sample rooms too
A factory may stop sandblasting on its own site. It could still buy a sandblasted effect from an outside finisher. Map every site that does the work.
Include small sample rooms, overflow suppliers and repair operations. Ask how each approved effect is produced and where the route records are held.
Use evidence suited to the risk. It may include a site review, equipment list and process records. Properly conducted worker interviews may also help. A supplier declaration is useful. If the route is unclear, seek other evidence too.
Compare the stated process with what the site can actually do. An effect may need equipment that is absent from the declared site. Ask for an explanation before drawing a conclusion.
Put route restrictions into purchase and subcontract documents. Make changes visible before production moves to another location.
Record which process and site each outside finisher is approved to use. Approval of a company alone does not approve every workshop it uses.
Support workers and review the first production period
Workers often know where the documented process differs from daily work. Ask them to help review the new route and what it asks them to do.
Train staff on changed tasks and protective controls. Cover defect handling and what to do when conditions are abnormal. It should also explain which old tasks are no longer permitted.
Review the workload and how the work area is set up. A new machine may lead to long periods of awkward manual finishing. That can create a new problem.
During early production, review quality and exposure-control records together. Include maintenance events and unplanned touch-up. A rise in one area may explain a change in another.
Set a review date. State which changes need an earlier review. A new fabric coating or chemical may trigger a review. So may altered extraction or a change of outside finisher.
Do not close the project merely because the first shipment leaves. Close it when the approved route works and the former process is retired. The continuing controls must have clear owners.
Frequently asked questions
Is changing from silica sand to another abrasive enough?
It may fail the buyer’s process rule. It does not remove every exposure. Check the actual rule and assess the whole substitute. Some buyers prohibit all abrasive blasting.
Is laser always the preferred replacement?
It is one candidate for certain effects. Test and approve the garment and installed controls. Check the remaining tasks and the complete route too. A technology name cannot replace that evidence.
What if the buyer rejects the new appearance?
Review which visual features are essential. Check whether another approved route or design change can meet them. Hold affected work when no approved solution exists.
Can old worker exposure be ignored after the change?
No. Ending a process does not erase past exposure. Qualified professionals should manage suitable occupational-health follow-up. They must follow the relevant requirements.
Keep a clear record of the final decision
A successful replacement removes the banned or hazardous operation. It puts a workable route in place and controls the risks that remain.
Link the effect brief and buyer rules to the exposure review. Add garment results, the approved route and evidence that the old process has ended. This record shows what changed and why it was accepted. It also states which conditions must remain in place.
References
NIOSH: Silica and worker health.
Levi Strauss & Co.: 2025 Supplier Code of Conduct Implementation Guidebook.
US EPA: Design for the Environment alternatives assessments.



Discussion0
Loading the discussion…